China United Mould

Logo 2021

Quality & Inspection

Quality

Inspection agreed before production starts

Our work is run under an ISO 9001 quality management system. Before production we agree the inspection plan for each casting with you: which dimensions are checked and how, which material tests are required, the NDT method and acceptance level for surface and internal defects, and the documents shipped with each lot. A common reference for industrial steel investment castings is ASTM A957, together with the material standard on the drawing.

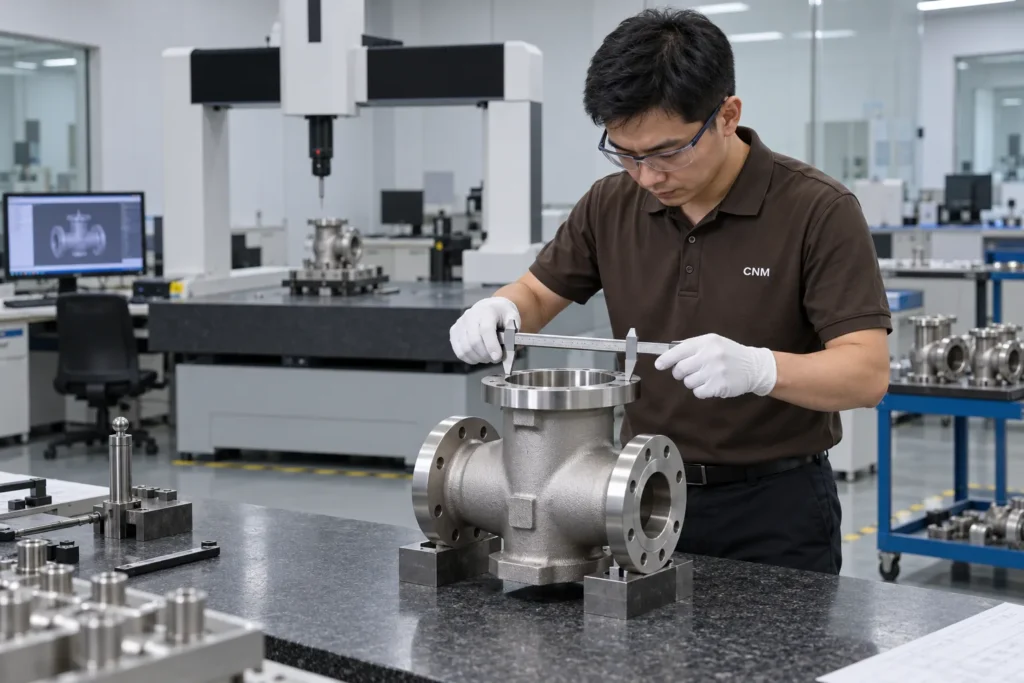
Inspector measuring a machined valve body casting on a granite table, CMM behind

Common inspection methods for investment castings

DimensionalFirst article inspection report against every drawing dimension; production checks with calipers, height gauges, go/no-go gauges, fixtures or CMM.
Chemical compositionOptical emission spectrometer (OES) analysis, typically one sample per heat, against the specified grade.
Mechanical propertiesTensile and hardness tests on separately cast or attached test bars, or hardness on the parts, after heat treatment.
Visual (VT)Surface condition against the agreed standard, for example MSS SP-55 for valve and fitting castings.
Penetrant (PT) and magnetic particle (MT)Surface-breaking defects. MT only works on magnetic grades such as carbon steel, 17-4PH and martensitic stainless; austenitic 304 and 316 castings are checked by PT.
Radiography (RT)Internal shrinkage, porosity and inclusions, graded against ASTM E446 or E192 reference radiographs where the specification calls for it.
Pressure tightnessHydrostatic or air leak testing of pressure-containing parts, where required.
DocumentsInspection reports and material certificates as agreed, for example an EN 10204 3.1 certificate with chemistry per heat.

Which tests apply depends on the part and its service, and is agreed per project.

Quality FAQ

Do you provide material certificates?

Material certificates and inspection reports are agreed per project, for example chemistry per heat and mechanical test results. Tell us the certificate type you need, such as EN 10204 3.1, when you ask for a quote.

How are internal defects controlled?

Mainly by design and gating: heavy sections are fed through the gate, and the gate position is agreed at the drawing review. Where the specification requires it, castings are radiographed and graded to the acceptance level on the drawing.

Have a casting in mind? Send us your drawing for a quotation.